Tool transfer
We take over and maintain your existing tools
Services
ACA Atlas Contacte designs and builds stamping tools in its own tool shop in Wehr (Baden), Germany: progressive dies for stamping presses and stamping and bending tools for stamping and bending machines. Tooling maintenance and modifications happen under the same roof as production.
01 Overview
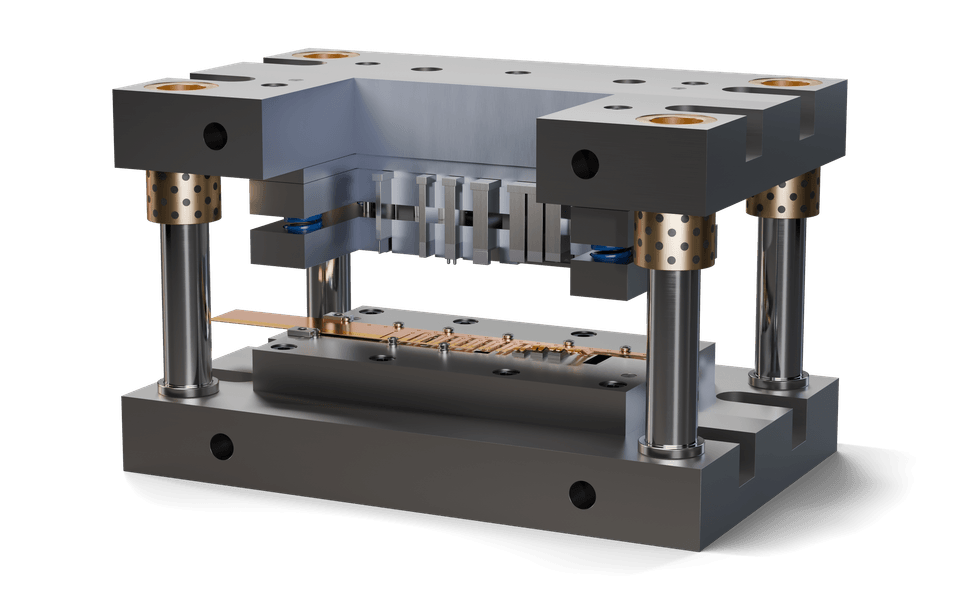
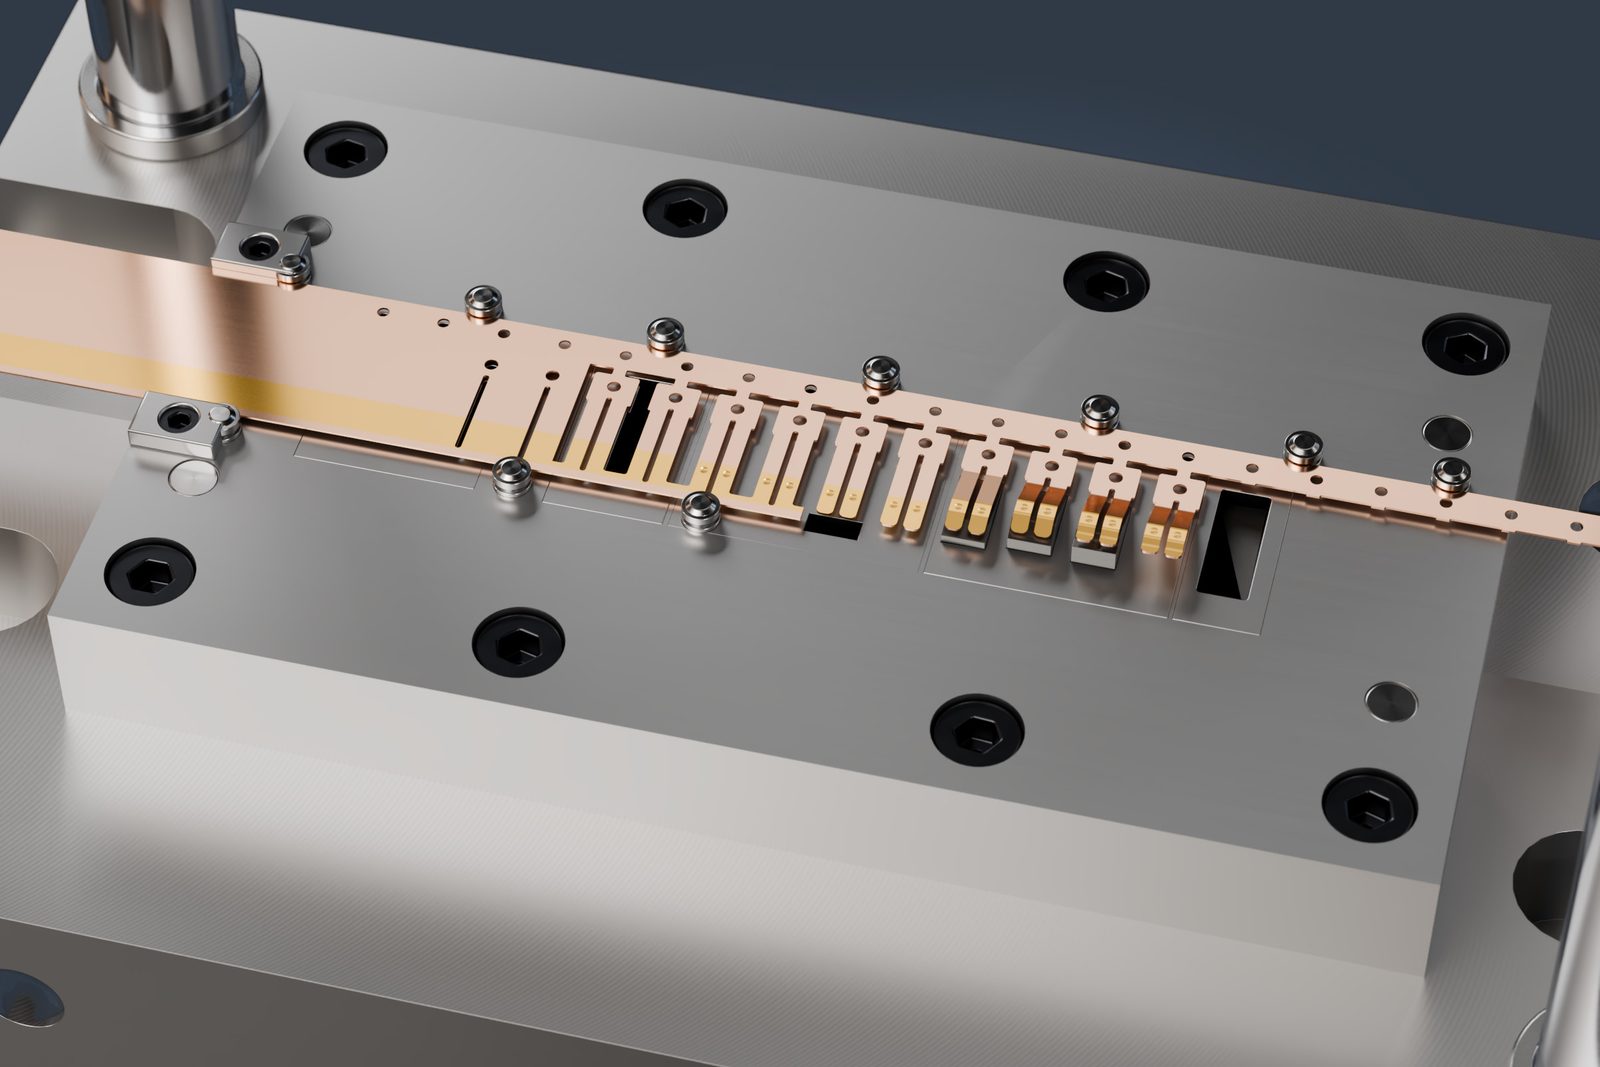
A stamping tool, such as a progressive die, is the most important production asset behind a stamped and bent part. It determines dimensional accuracy, burr formation and material utilisation, and with them the unit price over the entire series. At ACA it is built in our own tool shop, and it remains the responsibility of the toolmakers who built it throughout series production.
This pays off above all when something changes. A punch wears, your drawing gets a new revision, a feature needs a tighter tolerance. We modify the tool in-house, run it in again on the same machine and keep delivering. Tool making and production are under one roof.
The development of stamping and bending tools is part of the scope of our ISO 9001:2015 certification.
02 Tool types
| Criterion | Progressive die | Stamping and bending tool |
|---|---|---|
| Machine | Stamping press | Servo-controlled stamping and bending machine (multi-slide) with bending slides |
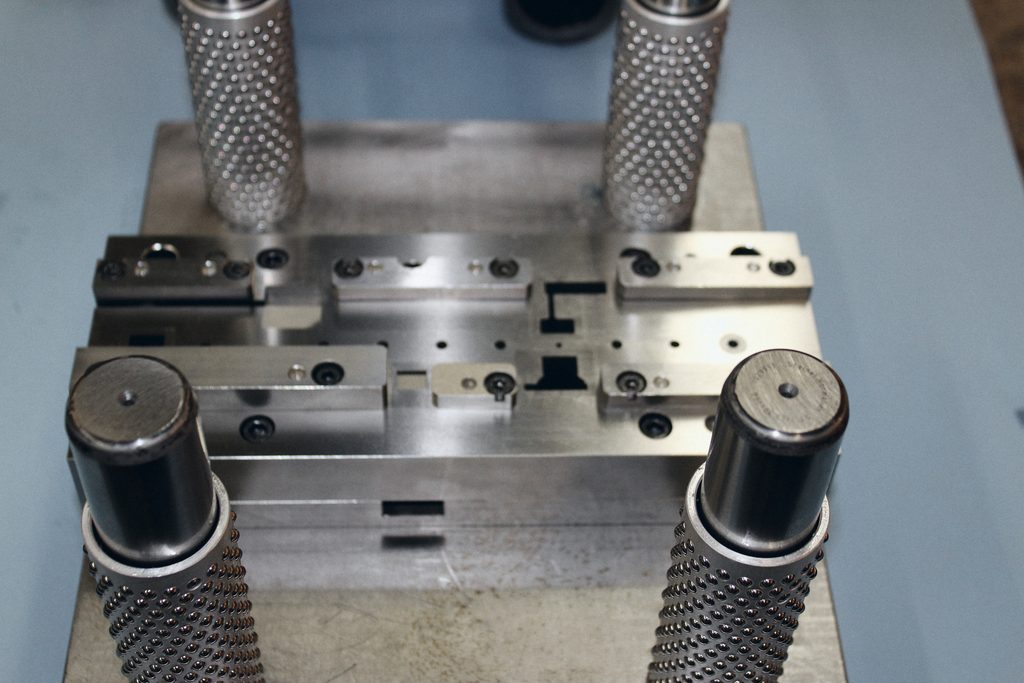
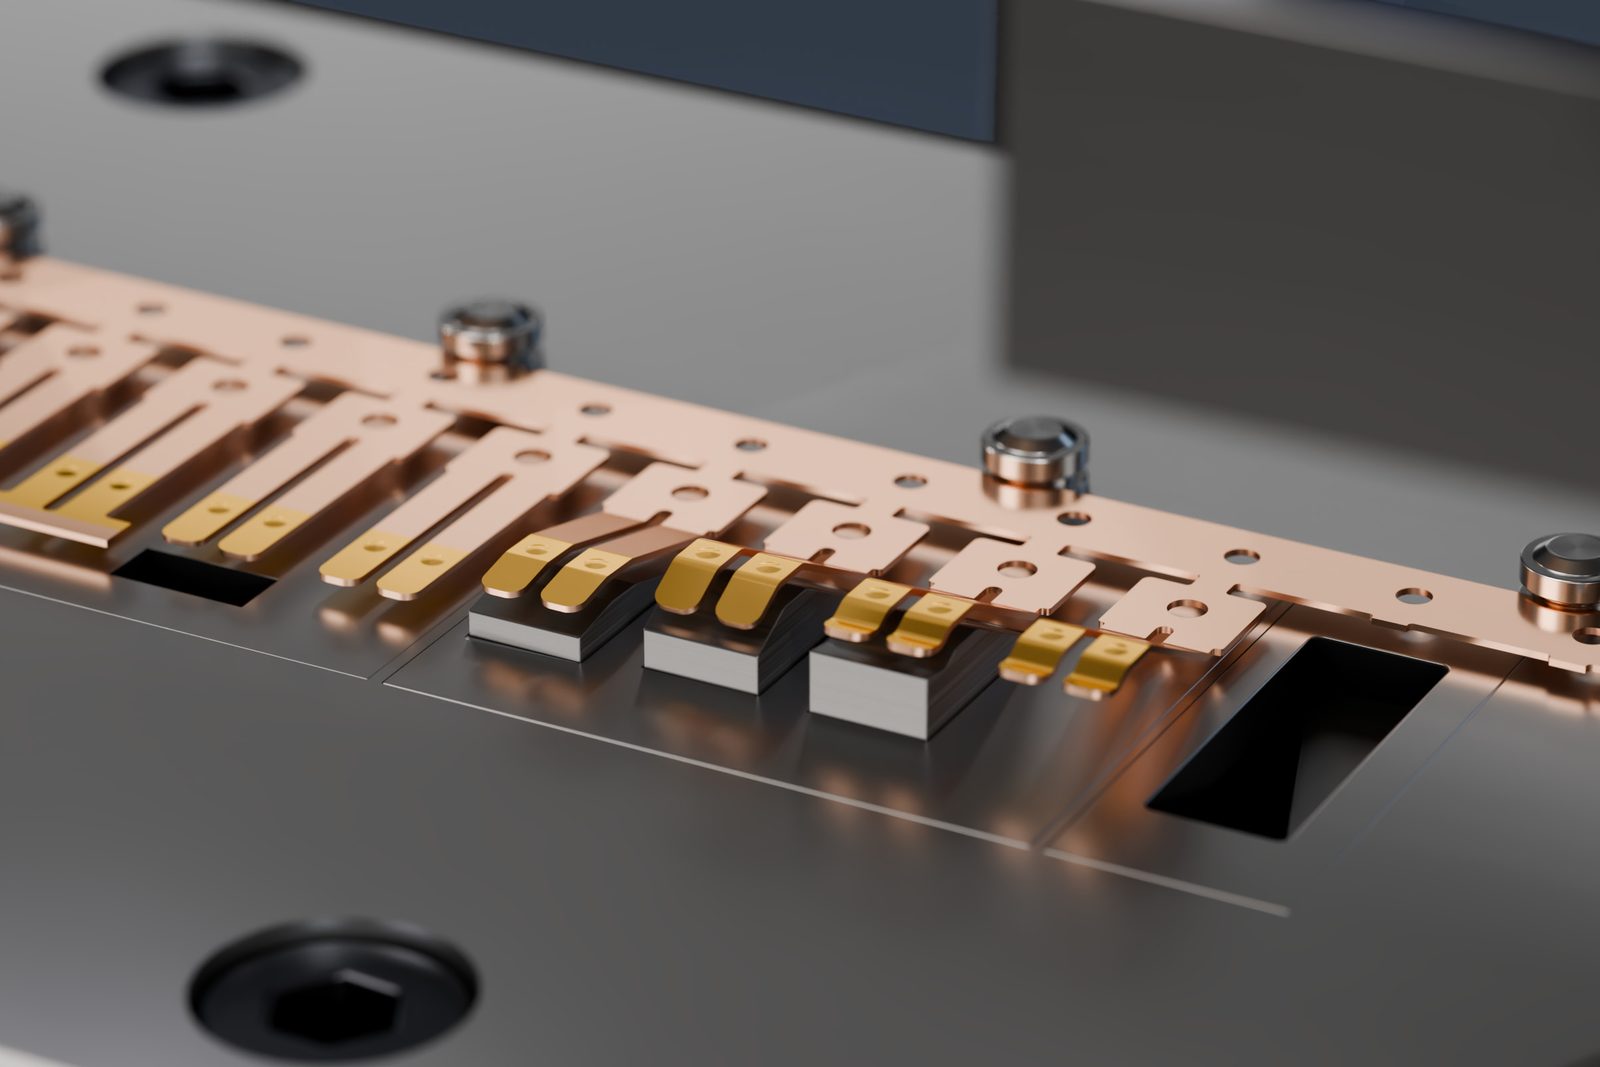
| Principle | The strip runs station by station through one tool: piercing, notching, coining, bending, cut-off. | Stamping takes place in the tool, bending is done by slides that work on the part from several directions. |
| Strengths | Consistent parts in high volumes, delivery on the carrier strip on reel possible | Complex three-dimensional bends, closed and rolled shapes, processing of strip and wire |
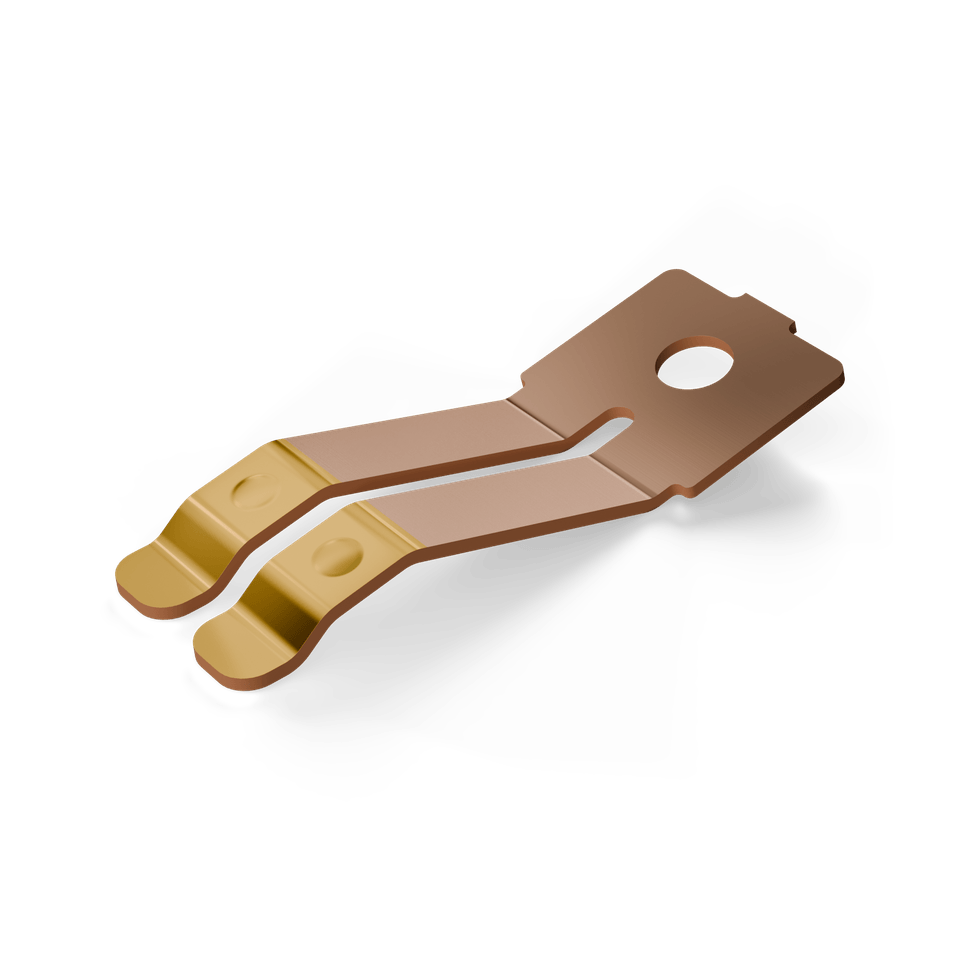
| Typical parts | Plug contacts, flat tabs, terminal parts, contact strips | Contact springs, clamping springs, rolled contacts, parts with multiple bends |
Which tool type is economical for your stamped and bent part depends on geometry, material and volume. We recommend a tool type with our quotation and explain why.
03 Process
From your part drawing we develop the flat pattern and the strip layout: which operation runs in which station, how the part is attached to the carrier strip and how much material is left over.
Cutting punches, dies, guides and bending stages are designed. Where it makes sense we build modular tools, so that variants and special versions can be produced with modified inserts.
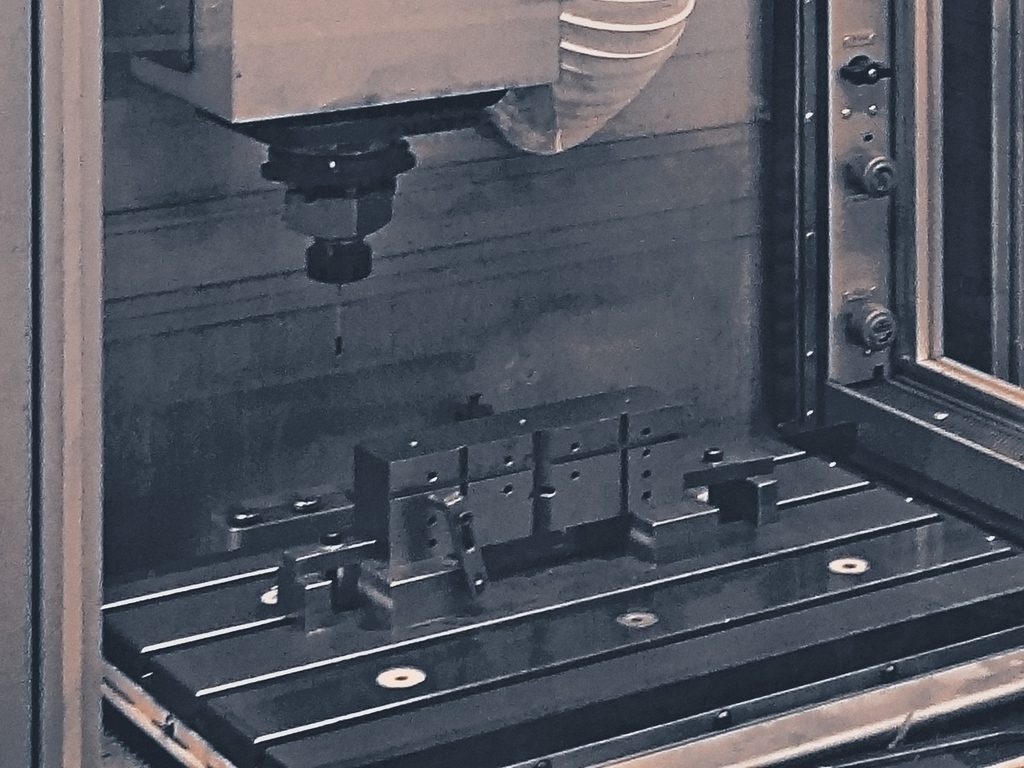
Contours are cut by EDM, plates and punches are milled and ground, inserts are fitted precisely.
The tool is run in on the production machine and the first parts are measured. On request we submit samples for your approval before series production starts.
During the series we maintain the tool, regrind cutting edges and replace wear parts before they become a problem.
04 Maintenance
A tool is not finished when series production starts. Cutting edges dull, the burr grows, springs and guides wear. At ACA, tool maintenance means that we watch burr and dimensions during the series, regrind cutting edges, replace wear parts and document every change made to the tool.
Drawing changes become tool modifications without bringing in an outside toolmaker. Tool costs and the storage of tools are governed by our general terms of sale (AVB, PDF in German).
05 Timeline
Set-up of the in-house tool shop with EDM technology.
New servo-controlled stamping and bending machines for strip and wire modernise production.
Two high-speed stamping presses add capacity.
06 Tool transfer
We do not only build new tools, we also take over existing ones. Whether your current supplier is closing down production or you want to qualify a second source, during a tooling transfer we inspect your tool, run it in, refurbish it where needed and take over series production.
FAQ
ACA Atlas Contacte builds progressive dies for stamping presses and stamping and bending tools for stamping and bending machines. Joining operations such as inline resistance welding of two-component parts can be integrated into the stamping process.
Yes. ACA Atlas Contacte maintains its tools in its own tool shop: regrinding, replacement of wear parts and modifications for a new drawing revision. Tool making and production work at the same site in Wehr (Baden), Germany.
ACA Atlas Contacte states the tool costs for your part in the quotation for your drawing. Tool costs, ownership and storage of tools are governed by the general terms of sale (AVB) of ACA Atlas Contacte, available as a PDF in German.
Build time depends on the number of stations, complexity and material. ACA Atlas Contacte states the date for tool and first parts with the quotation for your drawing.
We take over and maintain your existing tools
Design for manufacture from the first sketch
Made to drawing in steel, stainless steel and copper alloys
Request a quote
Send us the part drawing with material, finish and estimated annual volume. You will receive a quotation for tool and parts with a recommendation for the tool type.